

Product Details
-
Cast iron platform/flat plate series
-
Machine Tool Casting Series
-
3D Flexible Welding Platform Series
-
Granite and Marble Series
-
Ground rail groove rail series
-
Cast iron bending plate series
-
Square Box and Square Tube Series
-
Machine tool pad iron series
-
V-shaped frame series
-
Square ruler series
-
Skewner series
-
Magnesium aluminum alloy series
-
3D Platform Fixture Series
-
Ring gauge series
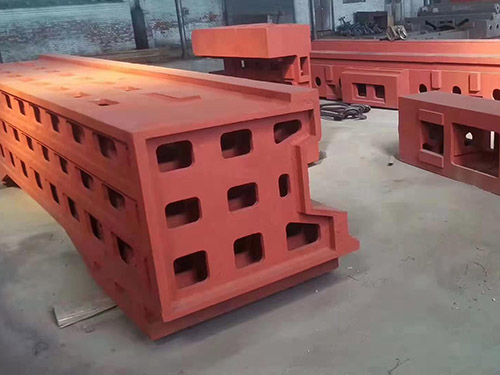
Large castings
Large castings: The fundamental focus of solving casting shrinkage defects is on "thermal balance".
The method for large castings is:
(1) Solidification is carried out at the thick and hot joints formed in the structure of machine tool castings, artificially creating a basic balance of temperature fields in various parts of the machine tool castings. Using internal and external cold iron, locally using zircon sand with high heat storage capacity, chromite sand or special coatings.
(2) Reasonable process design. The sprue is located at the relative wall of the machine tool casting, and is often numerous and scattered. Solidify the metal liquid that enters the thick walled area early and solidifies later in the thin walled area, achieving a basic equilibrium solidification in all areas. For machine tool castings with uniform wall thickness, multiple internal runners and air outlets are used. Multiple internal runners, dispersed and evenly distributed, ensure overall heat balance. The exhaust holes are thin and numerous, which not only ensures smooth exhaust but also plays a role in heat dissipation.
(3) Change the position of the internal pouring channel
(4) Choosing molding materials with high heat storage capacity is extremely important for producing wear-resistant products using lost foam molds! Replacing other types of sand with low heat storage such as quartz sand with chromite sand can achieve good results, with excellent microseismicity after pouring!
(5) Low temperature fast burning, open pouring system. Smooth and evenly fill the mold with molten metal. This should be tailored to the specific situation.
(6) The machine tool mold of ductile iron has high strength, surface hardness ≥ 90, and high rigidity of the sand box, which is beneficial for shrinkage.
(7) When a riser is needed, the first hot riser should be moved away from the hot node. If the riser is placed on the hot junction, it will inevitably increase the size of the riser, forming a "heat up heating". If not handled properly, not only will the shrinkage be difficult to remove, but it will also produce concentrated shrinkage holes, which will reduce the process yield.
(8) The tilted placement of molds and alloying both benefit. Shrinkage defects in machine tool castings are a complex process of understanding and implementation. The basic principle of "thermal balance" should be followed to analyze the casting of Ju body, formulate a reasonable process plan, select suitable molding materials, fixtures, and operate correctly and standardize. So any shrinkage defect in machine tool castings can be solved.
Main advantages of large castings
1. Large bed frame castings have accurate dimensions and shapes, good repeatability, and the characteristics of casting;
2. The surface smoothness of large bed castings is high;
3. Failure to fit the box or take out the mold simplifies the molding process, resulting in casting defects and waste of the machine tool bed caused by mold taking and box fitting;
4. Reasonable shaped sprues can be set at ideal positions, without being constrained by traditional factors such as parting and mold selection, reducing internal defects in castings;
5. Combination casting, with multiple pieces per box, improves the process yield and production efficiency of large machine tool castings;
6. Reduced processing allowance and lowered machining costs;
7. Adopt dry sand molding without binder, moisture, or any additives to prevent various casting defects and waste caused by moisture, additives, and binders;
8. The sand processing system has been simplified, and all molding sand can be reused, eliminating the need for molding sand preparation and waste sand treatment departments;
9. Large bed castings have no burrs or flying edges, reducing cleaning and polishing workload by more than 50%.
浙江Large castings 广东Large castings Recommended News
-
Core difference between ductile iron platform and ordinary cast iron platform (gray iron platform)
2026-05-26 10:14:51
-
How to judge the quality of cast iron parts? Teach you a few practical skills
2026-05-08 09:37:25
-
Why can't mechanical processing of cast iron platforms replace manual scraping and grinding for a lon
2026-04-22 02:32:46
-
Craftsmanship casting precision, Fengquan shines in Yongcheng - Hebei Fengquan Machinery shines at th
2026-03-26 01:49:33
-
The difference between HT-250 and HT-300
2026-03-11 09:42:53
CONTACT
—— Hotline:15733755098
—— Email:826899931@qq.com
—— Whatsapp:0317-8335666
—— Address:Xinhua Street, Jiaohe Town, Botou City